August 2026: From concept to hotel: precision lightweight concrete plant for innovative SVB room modules
From concept to hotel: Precision lightweight concrete plant for innovative SVB room modules
How state-of-the-art mixing technology is revolutionising the production of lightweight concrete room modules
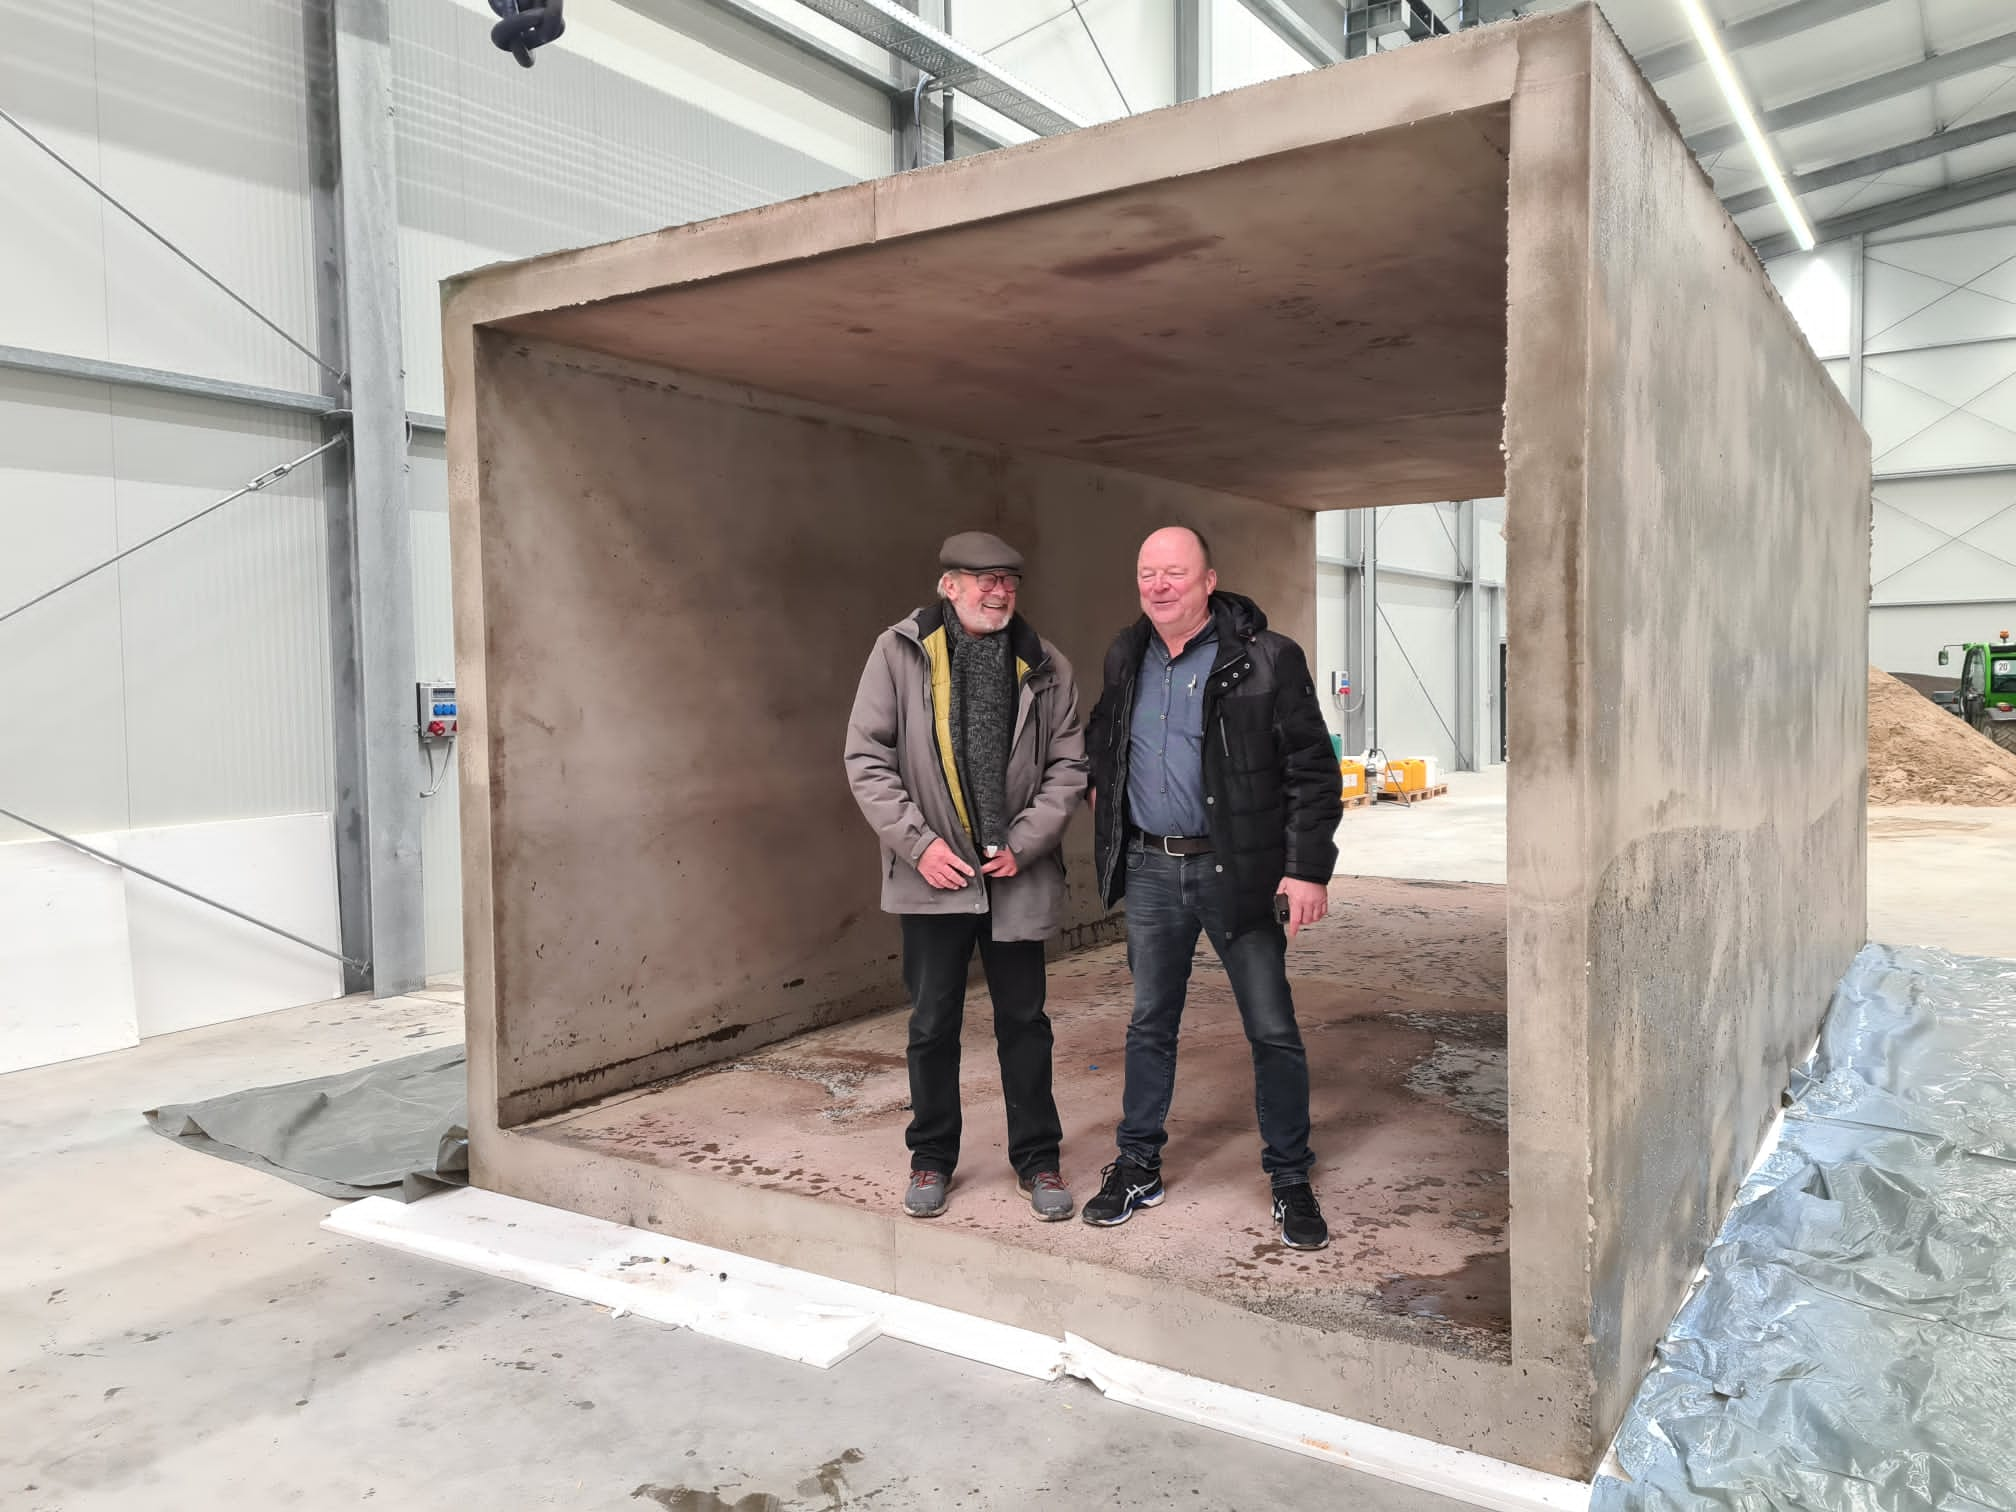
Demand for industrially manufactured room modules is growing steadily. In hotel construction in particular, short construction times, the highest quality standards and reproducible manufacturing processes are crucial factors for success. For a current hotel project, a state-of-the-art lightweight concrete plant with a capacity of 1.0 m³ was therefore developed and commissioned. The project impressively demonstrates how innovative mixing technology and well-designed plant engineering are taking the production of SVB lightweight concrete room modules to a new level.
Project timeline: From the first mixing trials to the finished hotel module
The foundations for this ambitious project were laid as early as the end of 2020. Once the contract was awarded, an intensive planning and development phase began.
In March 2021, extensive mixing trials were carried out at the University of Stuttgart. During these trials, a complete concrete mould was successfully filled. The insights gained formed the basis for subsequent series production.
Assembly of the plant began as early as April 2021. Following successful commissioning, the first room module made from SVB lightweight concrete was produced in January 2022.
A significant milestone was finally reached in November 2025: the construction of the first hotel using modular construction with the prefabricated Lightweight concrete room modules.
The heart of the plant: the Kniele KKM1000/1500 cone mixer
At the heart of the production process is the tried-and-tested Kniele KKM1000/1500 cone mixer with a high-quality ceramic lining. This model offers the ideal conditions for processing complex lightweight concrete mixes and ensures that all components are thoroughly blended.
The robust construction also ensures a long service life and minimises wear, even during continuous operation under demanding production conditions.
Maximum process reliability through intelligent weighing technology
Precise dosing of all raw materials plays a crucial role in quality assurance. The plant is equipped with a cement weigher featuring an integrated calibration device, which enables automated daily check weighing. Continuous monitoring ensures comprehensive logging of all production processes and guarantees the highest level of reproducibility of the formulations. At the same time, sources of error are reduced and quality standards are consistently maintained.
The system is supplemented by:
• Kniele water scale for precise water dosing
• Würschum additive scale for the exact dosing of additives
• Forced dust extraction from the mixer for clean and safe production
Efficient feeding and material supply
The material feed system has been specifically designed to meet the requirements of lightweight concrete production.
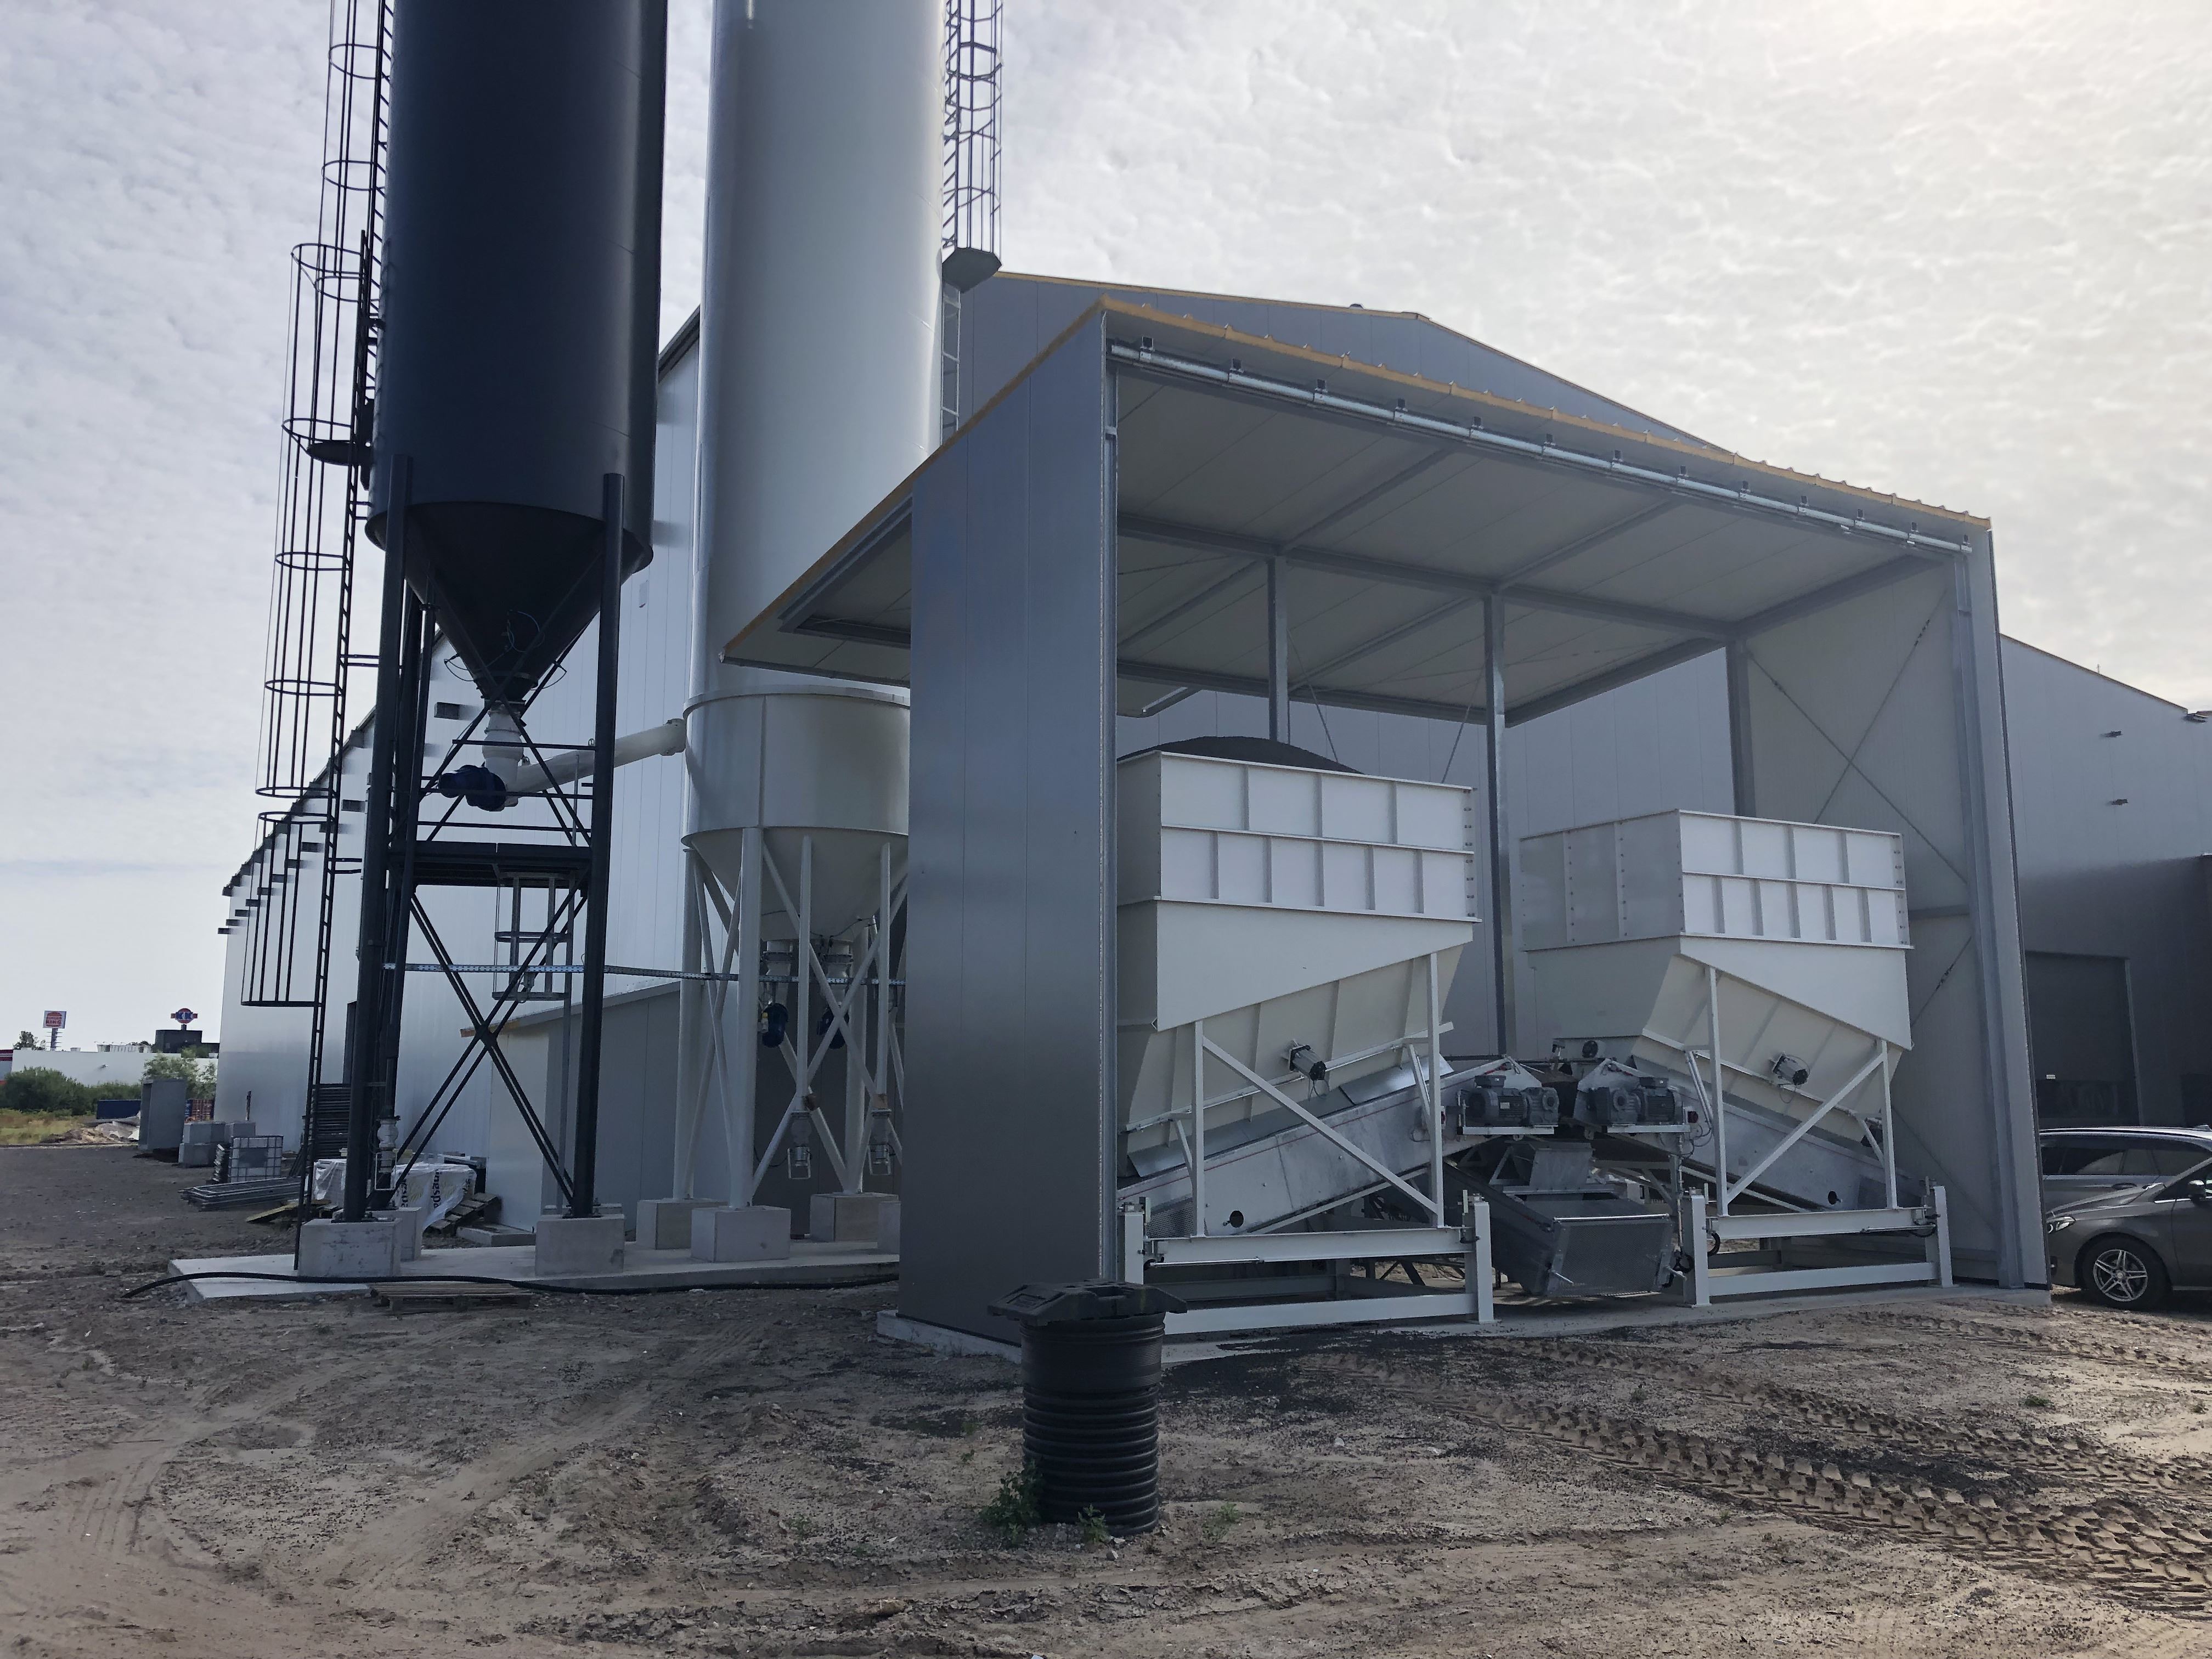
Two feed hoppers for the wheel loader handle the intake of raw materials. The materials are fed in a controlled manner to the inclined conveyor via measuring hoppers and discharge belts. A canopy reliably protects the aggregates from the elements.
To further optimise the process, a fibre dosing unit is integrated into the ascending conveyor. This enables fibres to be introduced into the production process precisely and consistently.
A total of three storage chambers are available for cement supply:
• 1 single-chamber silo
• 1 double-chamber silo
This flexible silo configuration allows for the storage of different binders and mix designs.
Well-designed logistics for concrete processing
After the mixing process, the concrete is conveyed via a WMW transport trolley. The system has space for two concrete drums at the same time, thereby enabling an efficient flow of materials within the production process.
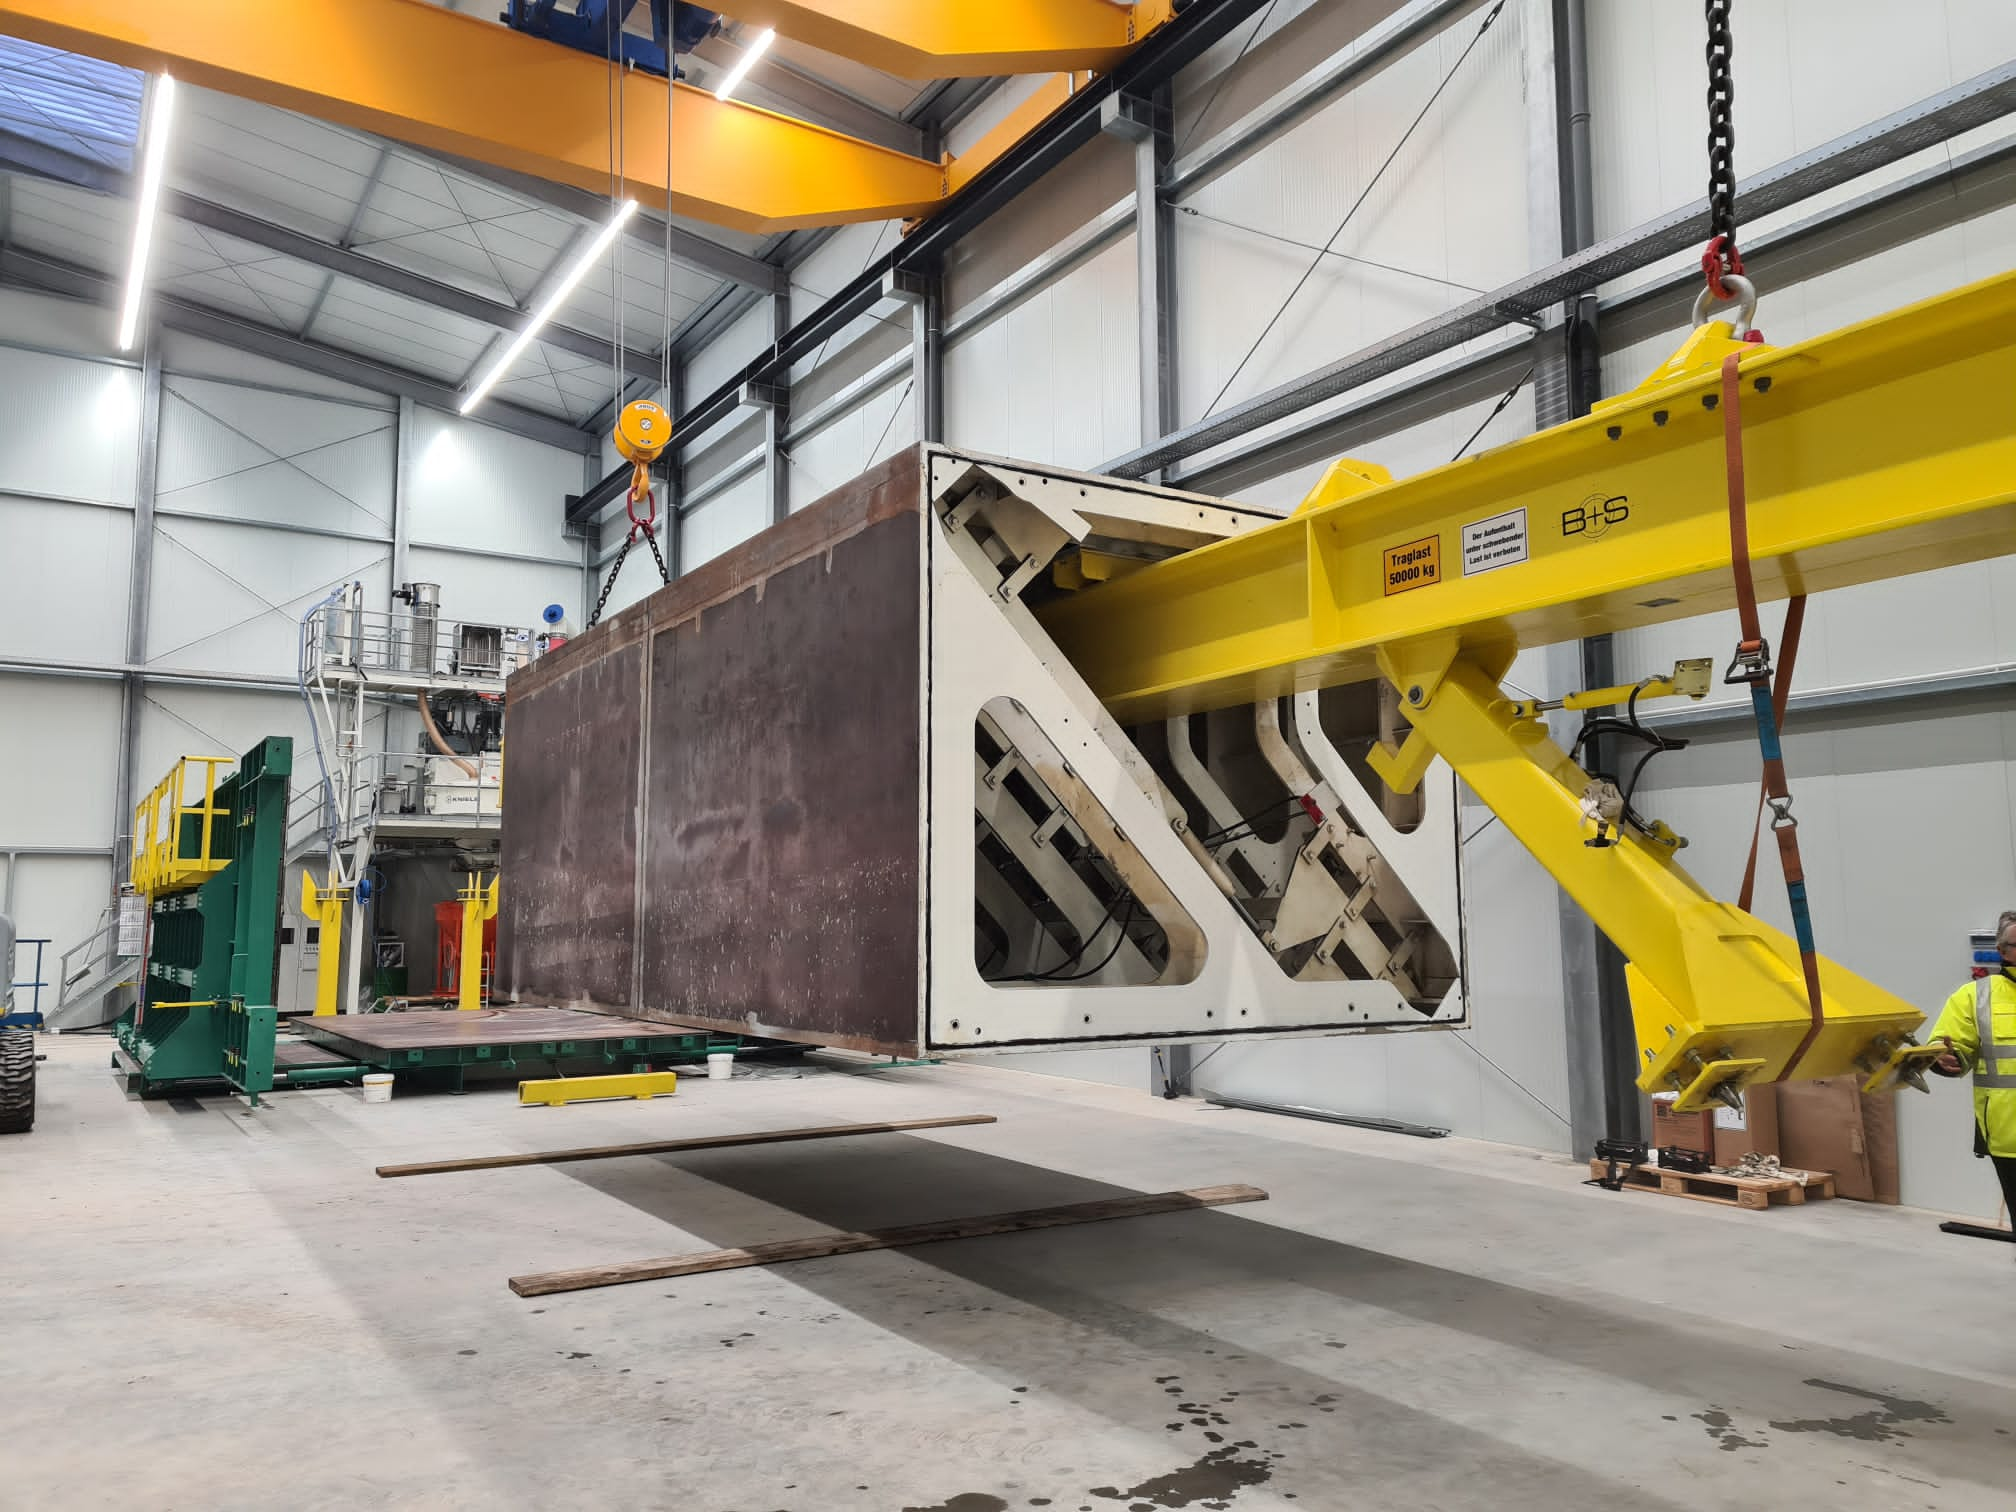
The moulds are then filled using a crane. This procedure ensures a precise and even distribution of the lightweight concrete within the large-format components.
Specialised concrete moulds for high-quality room modules
Specially developed concrete moulds from B+S are used in the manufacture of SVB lightweight concrete room modules. The bespoke moulding technology ensures a high degree of dimensional accuracy and supports the industrial production of complex room modules for modern hotel buildings.
Thanks to the combination of precise mixing technology, automated dosing and optimised moulding, the highest quality standards can be reliably met.
Conclusion: Future-proof lightweight concrete production for modular hotel construction
The lightweight concrete plant, with a capacity of 1.0 m³, exemplifies how modern plant technology and innovative manufacturing processes are shaping the future of modular construction. From the first mixing trial at the University of Stuttgart to the production of complete hotel room modules, a high-performance solution for the industrial production of SVB lightweight concrete has been developed.
With the Kniele KKM1000/1500 cone mixer, comprehensive quality assurance through automated weighing technology and well-designed plant logistics, the system offers the ideal conditions for the cost-effective, reproducible and high-quality production of lightweight concrete room modules in modern hotel construction.